


The resistance factor describes flow resistance as a dimensionless parameter and bridges theory and practice of flows in air, water, and hydraulic fluid. In the context of concrete demolition, rock cutting/processing, and special demolition, it influences pressure losses, energy demand, and working speed of hydraulic systems. For tools such as concrete demolition shears or hydraulic wedge splitters, a favorable resistance factor means: less power dissipation in the oil stream, lower heating, more stable forces, and reproducible cycle times. It is therefore a central planning and assessment criterion in connection with hydraulic power units for demolition, lines, quick couplings, and valves. As a compact sizing variable, it links calculation with field measurement via pressure and flow data and supports predictable commissioning, comparison of tool setups, and targeted troubleshooting across the full operating temperature window.
Definition: What is meant by the resistance factor?
In technical usage, the resistance factor mainly refers to two things: first, the drag coefficient of a body immersed in a flow (often called the cw value), which characterizes form and surface resistance in gases or liquids. Second, the resistance or loss coefficient in pipelines and fittings (often denoted ζ), which indicates how strongly local inserts, bends, valves, or couplings slow the flow and thus cause a pressure drop. In hydraulic drives – for example, when operating concrete demolition shears, combination shears, or splitting cylinders – the loss coefficient is decisive. It is directly related to the pressure drop, the flow velocity of the medium, the viscosity, and the line geometry. This is distinct from the friction factor along straight pipe runs, which describes the length-dependent portion of the pressure loss. Together, both quantities determine the effective power transfer from the hydraulic power pack to the tool and allow sizing of lines, valves, and couplings for stable operating points.
- ζ (loss coefficient): local loss at components; typical relationship: Δp_local = ζ × (ρ/2) × v^2.
- f (friction factor): length-dependent share; typical relationship: Δp_friction = f × (L/D) × (ρ/2) × v^2.
Application: resistance factor in hydraulics for demolition and splitting technology
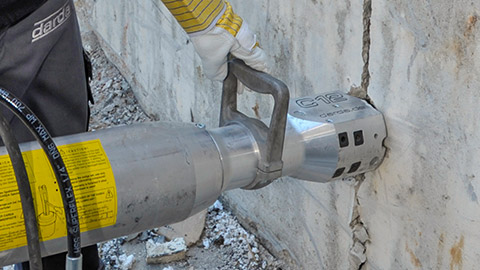
In hydraulic systems for concrete demolition and rock cutting/processing, the resistance factor describes the losses at local resistances: quick couplings, reducers, 90° bends, tees, valves, and transitions. The higher the resistance factor of these components at a given flow rate, the greater the drop in static pressure – causing heating, reduced effective force, and longer closing or spreading times. With concrete demolition shears this appears as slower cutting cycles; with hydraulic wedge splitters as lower piston speed of the splitting cylinder. A well-thought-out selection of line diameters, gentle changes in direction, suitable valve cross-sections, and high-quality quick couplings with a low resistance factor leads to stable working pressures, reproducible forces, and high operational safety – especially in continuous operation during gutting works, special demolition, natural stone extraction, or special deployments. In addition, return-line backpressure must be kept low because it reduces effective differential pressure at the actuator and can degrade cycle times even when the pressure line is correctly sized.
Influence on concrete demolition shears and hydraulic wedge splitters
The practical effect can be pinned down to two key questions: What flow rate does the tool require for the target speed, and how large are the resulting pressure losses in the hydraulic run?
Concrete demolition shears: cycle times and cutting force
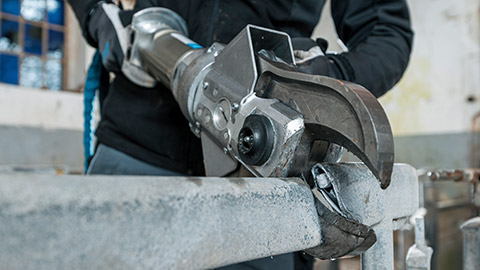
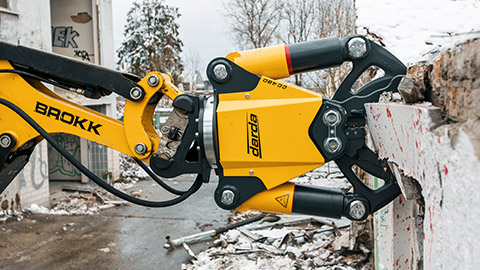
In concrete demolition shears, flow rate and pressure determine the closing and opening speed as well as the available cutting force in concrete and reinforcing steel. High resistance factors in lines or fittings reduce the pressure arriving at the tool and thus the force; at the same time, they extend the cycle time. The key is short, adequately sized hoses, large radii instead of sharp bends, and quick couplings with streamlined cross-sections. In practice, the available cutting force scales with the effective pressure at the cylinder area; every unnecessary Δp upstream reduces p_eff and therefore the cutting margin on heavily reinforced sections.
Hydraulic wedge splitters: piston movement and split pattern
In splitting cylinders, the pressure drop affects piston speed and response in the material. Low resistance factors support a smooth pressure ramp and reduce the risk of cavitation during retraction. The result is controlled splitting in concrete or rock – a benefit in tunnel construction, rock excavation, and natural stone extraction. Backpressure in the return path directly counteracts piston motion; a generously dimensioned, low-ζ return line is therefore as important as the pressure supply.
Flow fundamentals and calculation relationships
The pressure drop in a hydraulic line consists of length-dependent friction losses and local losses. The local losses are described via the resistance factor and increase with rising flow velocity. In practice, the relationship is often determined using known loss coefficients of the components, the density of the hydraulic fluid, and the volumetric flow rate. Since the flow rate influences velocity and thus dissipated power quadratically, careful sizing of cross-sections pays off – especially at high delivery rates for fast tools. Where data sheets list ζ values for fittings and couplings, a first estimate of Δp_local = ζ × (ρ/2) × v^2 combined with Δp_friction = f × (L/D) × (ρ/2) × v^2 helps to balance speed targets against acceptable heating.
- Key variables that drive pressure loss: volumetric flow Q, density ρ, internal diameter D, local coefficient ζ, and the friction factor f as a function of Reynolds number and roughness.
- Small reductions in D have a disproportionate effect because velocity v rises with Q/(A) and Δp scales with v^2.
Reynolds number, viscosity, and temperature
The flow characteristics in hydraulic lines depend strongly on viscosity and thus on oil temperature. As temperature rises, viscosity decreases, the flow becomes “more slippery”, and the length-dependent friction losses fall. At the same time, excessively low viscosities can adversely affect seals and leakage gaps. A stable thermal balance of the hydraulic power pack promotes consistent resistance factors and thus reproducible tool performance. Typical regimes: laminar flow at Re below roughly 2,300, transitional up to about 4,000, and turbulent above. In common pressure lines with mineral oil, operation is usually in the turbulent range; conversely, cold starts with high viscosity markedly increase Δp and can cause sluggish motion until the system warms to its target window.
Planning and design of hydraulic lines
A hydraulically “slim” run reduces resistance factors and saves energy. The following principles have proven effective in demolition, gutting, and tunnel construction:
- As few local resistances as possible (bends, tees, reducers); where necessary, large radii instead of 90° bends.
- Select line diameter by flow rate and permissible flow velocity; avoid unnecessary reductions.
- Use quick couplings with streamlined geometry; avoid cross-section constrictions due to contamination.
- Keep hose lengths short, avoid kinks and tight bend radii; employ swivel fittings deliberately.
- Size valves and control blocks by required Kv/flow; provide reserve capacity.
- Dimension return and case-drain lines generously to minimize backpressure at the tank connection.
- Minimize series chains of adapters and quick couplings; reduce the number of interfaces where feasible.
- Ensure cleanliness according to the specified contamination class; deposits and wear particles rapidly increase ζ at restrictions.
- Rule of thumb for flow velocities: pressure lines about 2 to 4 m/s, return lines about 1.5 to 3 m/s, suction lines about 0.5 to 1.2 m/s.
Typical fault patterns and diagnosis in operation
An unfavorable resistance factor rarely appears in isolation but as a chain of symptoms. Common signs:
- Noticeable oil heating without corresponding workload; decreasing tool speed after a short operating period.
- Delayed response of the concrete demolition shear when starting and finishing a cut; uneven running of the splitting cylinders.
- Pump noises, tendencies toward cavitation during retraction or when holding a load.
- Disproportionate pressure drops at the pressure gauge between power pack and tool as flow rate increases.
- Localized temperature hotspots at connectors or tight bends compared with adjacent hose sections.
- Audible flow hiss at throttling points; aerated or discolored oil in the sight glass after high-demand cycles.
- Rising energy consumption at unchanged duty profile and ambient conditions.
Pragmatic approach
- Compare flow and pressure at various measurement points (before/after couplings, valves, hoses).
- Identify constrictions step by step (couplings, reducers, filters) and replace them with more streamlined components.
- Check line cross-sections and lengths; where possible, increase radii and reduce deflections.
- Stabilize oil temperature during tests and document ambient conditions to ensure comparable readings.
- Change one parameter at a time and retest to isolate the influence on Δp and cycle time.
Fields of application: concrete demolition, gutting, rock excavation, and natural stone extraction
In all areas of application – from controlled concrete demolition and special deconstruction through gutting works to rock excavation and natural stone extraction – low resistance factors ensure targeted energy use. In special deployments with long hose bundles, additional valves, or tight workspaces, local losses often rise disproportionately; here, consistent optimization of flow paths pays off. Especially with concrete demolition shears and hydraulic wedge splitters, consistent tool performance is essential for precise cuts, controlled split patterns, and predictable cycle times. Extended umbilicals in underground or remote work sites particularly benefit from low-ζ components to maintain speed and reduce heat load.
Distinction: drag coefficient and pipeline resistance
The drag coefficient (cw) characterizes the resistance of a body in a flowing medium and is relevant in the construction sector, for example for wind loads on components or transported elements. In hydraulic drives, however, loss coefficients of lines and fittings dominate. For the design of hydraulic power packs, control blocks, and hose systems, the resistance factor as a loss coefficient is therefore the decisive tool, whereas the cw value is more peripheral and primarily associated with external rather than internal flow.
Safety, efficiency, and service life
Low resistance factors reduce waste heat, slow oil aging, and support stable sealing conditions. This has a positive effect on the service life of hydraulic components and tools. At the same time, an efficient flow cross-section improves the acoustic situation, minimizes cavitation, and reduces risks due to thermal overload. Observance of component pressure ratings, minimum bend radii, and correct tightening torques at connections contributes to reliability, as does suitable monitoring of temperature and pressure where applicable. The statements here are general and do not replace an assessment of the specific case in compliance with the applicable regulations.
Practical recommendations for optimization
- Hydraulic power packs with sufficient flow rate and heat management; maintain the hydraulic oil’s temperature window.
- Lines/couplings check for streamlined geometry; rule out wear and contamination as causes of cross-section losses.
- Tool matching between power pack, control, and concrete demolition shear or splitter; harmonize flow rate and pressure requirement.
- Documentation of measured values (pressure, temperature, flow) to detect changes of the resistance factor in operation.
- Commissioning with an acceptance checklist including target pressure drops per section and defined tolerance bands for cycle times.
- Condition monitoring via periodic flow and pressure testing with calibrated equipment to enable trend analysis and preventive maintenance.
This page may be cited in commercial and non-commercial publications (e.g., specialist publications, forums, or social media) without prior permission.
Please feel free to copy the following link for your quote.