


Negative formwork refers to the deliberate creation of recesses, depressions, and reliefs in concrete using a matching counter-mold. It is used in building and structural engineering, precast production, and tunnel construction – from service niches and penetrations to textured fair-faced concrete surfaces. In planning, production, and later modification, this brings together formwork, reinforcement routing, surface technology, and – when adapting existing structures – selective removal methods. For controlled corrections at component edges and openings, practitioners commonly use, among other tools, concrete pulverizers and hydraulic rock and concrete splitters when low-vibration and precise interventions are required. In practice, negative formwork is also termed recess formers or blockouts when defining cavities and openings for later installations.
Definition: What is meant by negative formwork?
Negative formwork comprises formwork and form parts that, as a negative geometry, reproduce the later recess or hollow shape in the concrete. This includes void formers, inserts and embedded-part geometries, elastic form liners/matrices for surface textures, and sacrificial (lost) formwork. This is distinct from “positive” formwork, which shapes the external contour of a component. The aim is a dimensionally accurate, tight, and easily demouldable form that safely transfers the fresh concrete pressure, produces the required surface, and enables code-compliant reinforcement routing around the recess. Clearly defining whether elements are temporary (to be removed) or permanent (to remain as lost formwork) is essential for durability and inspection.
Function, configuration, and materials of negative formwork
Negative formwork transfers fresh concrete pressure into the main formwork or into the supporting falsework. Critical factors are stiffness, tightness, demouldability, and stable fixation during concreting. Common materials include wood-based products, steel, aluminum, plastics, and elastomeric form liners; for void formers also foams or lightweight composite materials. Release agents must be compatible so the form separates cleanly and no pore patterns or marks arise.
- Selection criteria in practice: load-bearing capacity under fresh-concrete pressure, dimensional stability, and resistance to vibration.
- Sealing concept: butt joints, penetrations, and transitions must be sealed to prevent laitance leakage and edge honeycombing.
- Service finish: target surface class, texture depth, and joint layout determine the liner grade and backing support.
- Material compatibility: alkali resistance, heat behavior, and reaction to release agents influence reuse and color stability.
- Lifecycle view: reusability versus sacrificial design, waste volume, and recyclability of components.
Void formers and sacrificial parts
Void formers are bolted, welded, bonded, or mechanically clamped and removed after hardening. Depending on requirements, inserts may remain in place as lost formwork within the component. For penetrations and anchor zones, crisp edges, chamfers, and sufficient edge distance are important to avoid spalling.
- Provide chamfers or fillets at corners to reduce stress concentrations and improve stripping behavior.
- Use preformed edge profiles for repeatable dimensions when many identical recesses are required.
- Plan venting and filling paths to avoid air entrapment behind large void formers.
Form liners for surfaces
Elastic matrices create reliefs, ribs, and textures on fair-faced concrete surfaces. They must lie flat, be tightly sealed, and be well supported. The concrete mix design (aggregate grading, slump flow) and the degree of concrete compaction significantly influence the imprint of the negative form.
- Common issues and mitigation: air voids in deep textures – use targeted vibration and consider self-compacting mixes.
- Visible liner joints – align and seal joints consistently with the architectural grid.
- Liner creep or deformation – provide continuous backing and limit temperature exposure.
- Staining from release agents – test on mock-ups and dose sparingly and uniformly.
Planning, structural analysis, and reinforcement routing around recesses
Recesses alter load paths. Notch effects, shear stresses, and crack widths must be considered; reinforcement must be routed, concentrated, and anchored. Minimum cover, distances to component edges, and the use of chamfers reduce spalling. Dimensional and positional tolerances, surface classes, and joint layouts are clearly defined already in the execution planning.
- Coordinate early with building services to avoid clashes and late relocations.
- Model recesses and embedded parts in 3D to verify cover, anchorage, and collision clearance.
- Define inspection hold points, acceptance criteria, and documentation duties in the method statement.
- Assess effects on fire resistance, watertightness, and acoustic or thermal performance where relevant.
Tolerances and dimensional accuracy
Negative formwork must be positioned accurately in shape and location. Control points, auxiliary templates, and pre-run mock-ups help avoid fit inaccuracies. In precast production, a check frame ensures repeat accuracy.
Use total-station layouts or calibrated templates for positioning, measure critical dimensions immediately after stripping, and document as-built conditions for traceability. Where required, 3D scanning supports verification of complex reliefs.
Execution: assembly, concreting, and stripping
Assembly is carried out stress-free and with full load transfer; penetrations must be sealed to prevent washouts. During concreting, concreting speed, drop height, and compaction intensity must be chosen so the negative form is neither displaced nor overstressed. Stripping times depend on component thickness, cement type, temperature, and the required surface quality. Damage often occurs during stripping – therefore work slowly, evenly, and with suitable levering and pulling directions.
- Place concrete in layers with controlled drop height to avoid liner uplift or local overstress.
- Apply internal vibration close to recess edges with limited contact to liners; avoid over-vibration.
- Check fasteners and braces before each lift; re-tighten if settlement occurs.
- In hot or cold weather, adapt curing and stripping to maintain edge integrity and surface class.
Quality assurance
Visual inspection for tightness, positional control, reinforcement approval, documentation of concreting sections, and weather conditions are part of quality assurance. For textured surfaces, reference fields are helpful.
- Verify recess geometry, squareness, and edge sharpness including specified chamfers.
- Check continuity of textures across panel joints and consistent pore patterns.
- Confirm clearances to embedded parts and minimum cover prior to concreting.
- Record release agent product and dosage to ensure reproducibility.
Subsequent openings, adjustments, and deconstruction around negative formwork
Despite careful planning, subsequent adjustments are common: openings are enlarged, recesses relocated, or edges reworked. In existing structures and during concrete demolition and special demolition, low-vibration and controlled methods are required to protect adjacent components, embedded parts, and fair-faced concrete surfaces. In building gutting and concrete cutting, low-dust and low-noise steps are key.
Tools and methods for precise removal
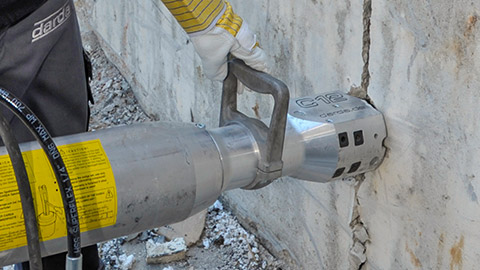
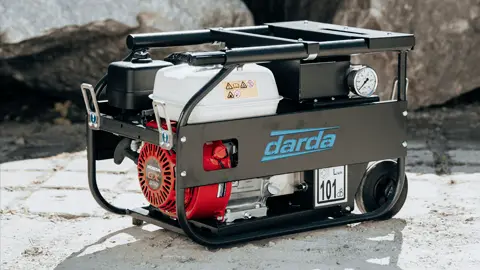
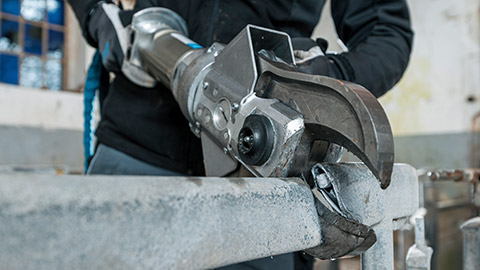
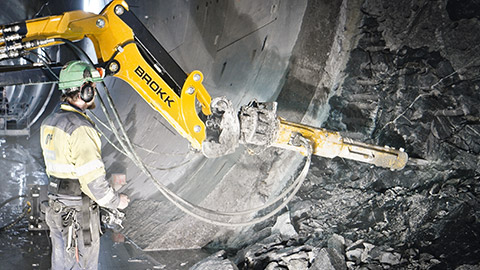
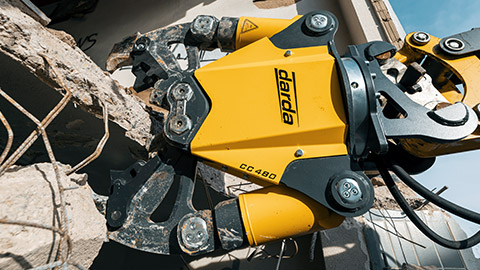
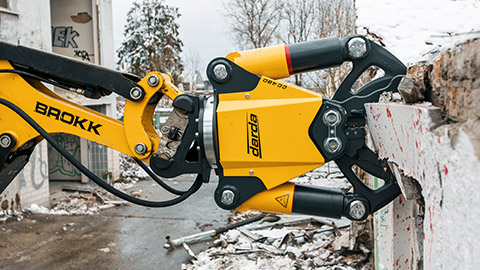
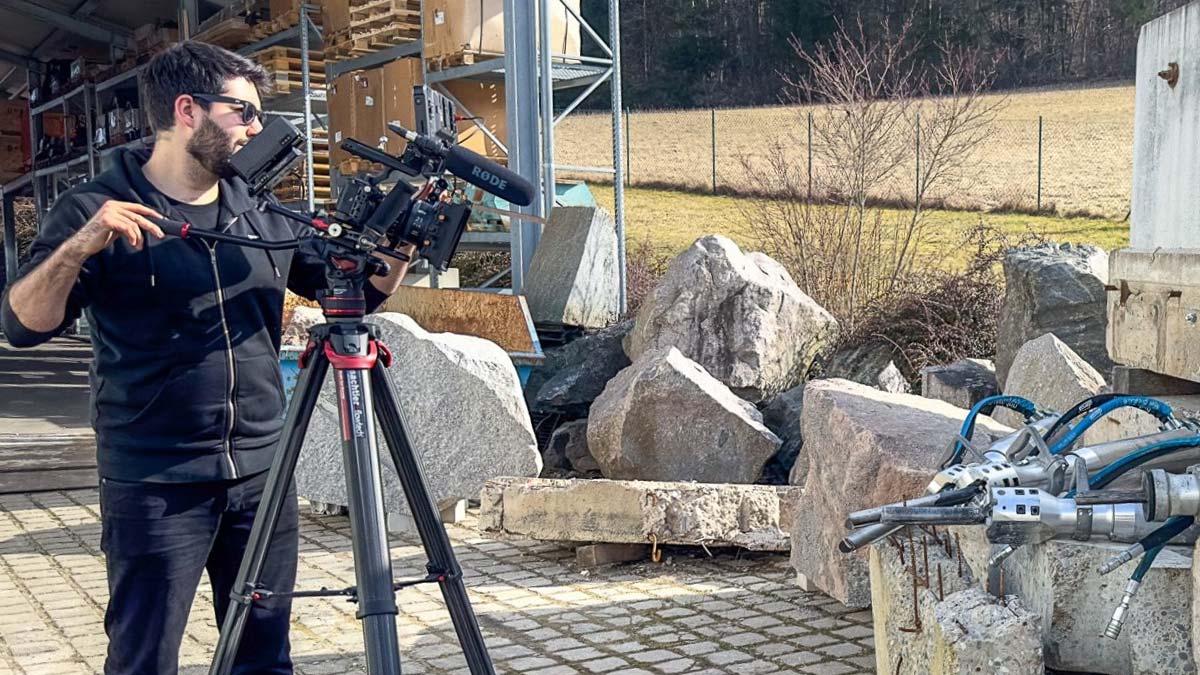
Concrete pulverizers enable edge-friendly, controlled breaking out of concrete parts – for example, when exposing embedded parts in or next to negative formwork, removing defects, or carefully enlarging recesses. Hydraulic wedge splitters create separating cracks along defined borehole rows; the resulting fracture surfaces follow the stress field and reduce vibrations, which is advantageous in vibration-sensitive environments. Compact hydraulic power units reliably supply these tools with energy, even under confined construction-site conditions. Where reinforcement must be severed, Multi cutters, steel shear, or hydraulic demolition shear support clean separation. In metal-dominated special installations, depending on the task, specialized tools such as a cutting torch may be used. These approaches are particularly relevant in rock demolition and tunnel construction when niches need to be precisely adjusted later in segments or inner linings.
Combining splitting along borehole rows with subsequent localized pulverizing often lowers peak vibrations and provides clean, predictable edges.
Steps for creating a subsequent recess
- Define geometry: perform structural analysis, locate utilities, consider edge distances and reinforcement.
- Secure the work environment: dust and debris protection, shoring, barriers, prefer low-emission methods.
- Preparation: mark out; if necessary, perform core drilling for guidance and stress relief.
- Separation/removal: remove section-wise with concrete pulverizers or split in a targeted manner with hydraulic wedge splitters; protect edges.
- Sever reinforcement: depending on diameter, use steel shear, Multi cutters, or hydraulic demolition shear.
- Finishing: add chamfers, blend surfaces, gently clean fair-faced concrete surfaces.
- Disposal and documentation: separate material fractions, provide proof, update as-built data.
Notes on occupational safety and methods are general in nature and do not replace project-specific planning.
Use cases: from fair-faced concrete to tunnel construction
Negative formwork shapes equipment niches, access openings, and reliefs in buildings and infrastructure structures. In precast production, matrices provide recurring surface textures. In tunnel construction, niches, roundings, and blockouts in segments and inner linings are realized with robust negative forms; later adjustments are often selective – e.g., with concrete pulverizers or hydraulic wedge splitters – to minimize vibrations. In building gutting and concrete cutting, this preserves the load-bearing structure while exposing embedded parts. In special-use scenarios, for example during ongoing operations, low-noise, controllable methods are crucial.
Digitally coordinated recess data in design can be transferred to fabrication templates in precast plants to improve repeatability and reduce rework.
Special requirements in existing structures
Existing-structure situations often require dust and vibration limitation, edge stabilization at fair-faced surfaces, and precise control of fracture lines. Here, the combination of careful preplanning of intervention edges and hydraulically supported, finely metered tools is key.
Where sensitive neighbors or equipment are present, define vibration and noise thresholds, monitor during execution, and apply water or extraction systems to control fine dust.
Fair-faced concrete and design with negative formwork
For textured surfaces, the interaction of matrix geometry, concrete mix design, placement technique, and curing determines the result. Uniform pore patterns, sharp edges despite chamfers, and reproducible relief sharpness are supported by defined fresh concrete consistencies, tuned compaction, and correctly dosed release agents. For durability, edge sealing, suitable curing, and protection against early damage are essential.
- Align liner joints with the architectural grid; decide on intentional visibility or concealment of seams.
- Keep liner orientation consistent to avoid directional gloss or texture misalignment.
- Use compatible repair mortars and surface treatments for local touch-ups without color shifts.
- Protect fresh textures from runoff, impact, and early dehydration until sufficient strength is reached.
Occupational safety, environment, and disposal
During production and deconstruction in the context of negative formwork, pay attention to load transfer, safe handling, and dust and noise reduction. Low-vibration methods reduce risks to adjacent components and sensitive areas. Separating material fractions facilitates environmentally sound disposal; water and fine dust ingress should be minimized.
- Control respirable dust and noise exposure with suitable engineering controls and PPE.
- Plan lifting points and handling aids for heavy form parts to avoid manual handling injuries.
- Collect process water and fines; prevent uncontrolled discharge into soil or drainage systems.
- Prefer reusable form parts and recyclable materials to cut waste.
Typical mistakes and how to avoid them
- Leaky joints at the negative form lead to washouts – seal all butt joints before concreting.
- Warped void formers cause dimensional errors – brace and fix adequately.
- Spalling during stripping – provide chamfers, observe appropriate stripping times, relieve loads.
- Unsuitable release agents – use only compatible agents in the correct quantity.
- Insufficient reinforcement routing – consider notch effects, prove re-direction and anchorage.
- Missing venting behind large formers – provide vents or controlled filling to prevent air pockets.
- Over-vibration near liners – adjust technique to preserve texture and avoid segregation.
This page may be cited in commercial and non-commercial publications (e.g., specialist publications, forums, or social media) without prior permission.
Please feel free to copy the following link for your quote.